Specifications and evidence · Technical buyers
How to Set Practical Dimensional Tolerances for Shisha Charcoal Cubes
Define the size limits and the receiving check together. Match tolerances to packaging and HMD needs, then agree how damaged pieces and borderline readings will be handled.
Target and limitsMeasurement and samplingFit and acceptance
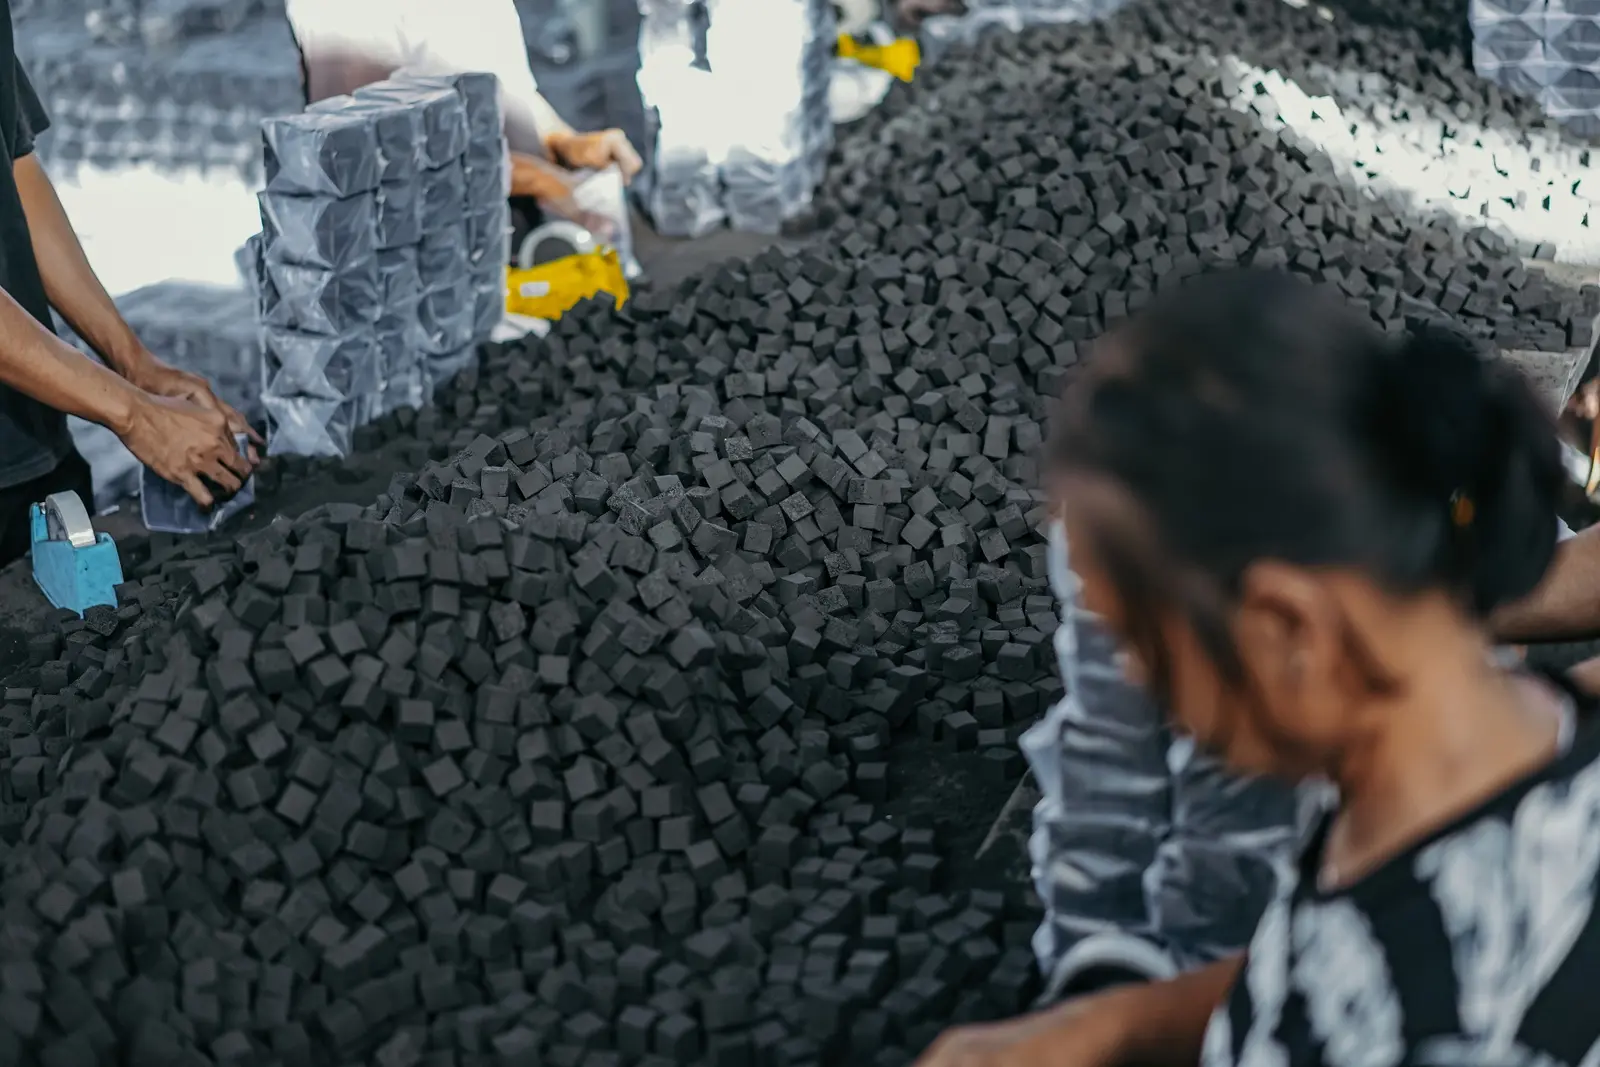
Shisha charcoal cube size tolerance
A tolerance needs limits, a method and a decision rule.
Nominal size is a target description. Minimum and maximum limits establish the allowed dimensional range under an agreed measurement procedure.
Agree sample selection, measurement points and damage treatment before inspecting the delivery. Check the actual packaging and HMD fit separately.
Tolerance illustration only
Translate a stated allowance into explicit limits.
Illustrative target: 25.0 mm with an allowance of ±0.5 mm gives a minimum of 24.5 mm and a maximum of 25.5 mm.
These invented limits are not Unimax specifications or a recommended tolerance. State whether the limits apply to length, width and height individually, and define measurement points, sampling and the rule for readings near either limit.
Dimensional tolerance checklist
Agree these fields before receipt inspection.
| Review item | Question to resolve | Evidence / status / action |
|---|---|---|
| Nominal / limits | Length, width and height in mm; minimum and maximum for each relevant dimension. | __________ |
| Functional scope | Actual packaging arrangement, HMD or foil setup and fit criterion. | __________ |
| Measurement points | Axis orientation, jaw contact, positions and treatment of uneven faces. | __________ |
| Instrument / precision | Identity, resolution, verification, reporting precision and uncertainty handling. | __________ |
| Sample population | Lot and packs, sample count, selection method and sample condition. | __________ |
| Per-piece record | Individual readings, chips, cracks, missing material and photographs. | __________ |
| Acceptance / action | Decision rule, borderline review, out-of-limit count and escalation. | __________ |
| Approval reference | Current document version, order, sample and exception authority. | __________ |
Comparison rule: apply the agreed dimensional limits, measurement method, sample plan and decision rule. Keep damage and practical fit evidence identifiable.
01 · Nominal size and limits
A target size is not an acceptance rule.
A nominal cube size identifies the intended format. It does not, by itself, say how much variation is allowed. A useful specification identifies length, width and height in millimetres, with separate minimum and maximum limits for each dimension where needed.
Distinguish a manufacturing target from the limits used to judge a received sample. A typical or average size is not automatically a guaranteed limit. Ask whether conformity applies to each inspected piece, a sample statistic or another explicitly defined rule.
A statement such as “exact size, zero tolerance” leaves no stated allowance for production variation or measurement uncertainty. It can turn small differences between operators into a dispute. Agree realistic limits from function and manufacturing evidence rather than assuming extra decimal places make an order safer.
02 · Fit before numbers
Build the tolerance around the intended pack and setup.
Check the buyer’s actual HMD or foil arrangement, cube quantity, spacing and handling method. Where a device imposes a physical clearance, identify the relevant dimension and verify fit with representative samples. Do not assume one nominal cube format fits every HMD.
For packaging, check the planned row arrangement, liner, divider and usable internal dimensions. Cubes at the upper dimensional limit can challenge a tight pack; variation or damage can affect alignment. Test the proposed combination rather than deriving carton capacity from a nominal label alone.
Agree the usable condition and observation criteria for a practical trial. Fit is a physical check, while ignition and useful heat need separate evaluation. A dimensionally conforming cube does not independently prove complete product quality or satisfactory session performance.
03 · Measurement definition
Specify where the caliper touches the cube.
Identify the three axes and the measurement positions on each pair of opposite faces. Use a consistent orientation, light contact and jaw alignment. Avoid squeezing the charcoal or letting loose powder dictate contact; record any agreed preparation instead of changing the sample silently.
If faces are uneven, take readings at the agreed positions and keep them individually. Decide beforehand whether each reading must meet the limit or whether a defined representative result is used. A convenient average can hide a locally oversized face or an undersized damaged region.
Photograph the measurement arrangement and label cube identifiers. Separate intact-face dimensions from corner chips, cracks and missing material. If damage prevents the agreed measurement, record that condition and follow the damage rule rather than inventing a replacement dimension.
04 · Instrument capability
Resolution is only one part of a reliable reading.
Record the instrument identity, display resolution and verification or calibration status appropriate to the decision. Check zero and relevant reference dimensions, clean the contact faces and use stable measurement conditions. Use an instrument and procedure capable of resolving the proposed tolerance.
A fine display increment does not establish the same level of accuracy. Contact force, alignment, surface condition and operator repeatability also matter. NPL’s calliper guidance covers instrument use, measurement force and uncertainty; these general principles are relevant when designing a buyer procedure.
For close results, retain unrounded readings where available and agree the reporting precision. Do not round a marginal value into compliance or tighten the limits after seeing the data. Ask for qualified measurement support if the proposed limits exceed what the receiving check can reliably distinguish.
05 · Sampling and record
Define the inspected population before selecting cubes.
Agree the number of pieces and how they are selected across the relevant packs or lot. State which delivery or sample population the result represents. There is no universal sample count supplied by this guide; the plan should reflect the order scope and agreed inspection risk.
Record pack and lot references, sample condition, selection procedure, date and operator. Keep per-piece length, width and height readings with damage observations. Summaries such as mean and range can help review consistency, but cannot replace individual results when the acceptance rule applies to individual pieces.
Define how out-of-limit pieces, unreadable damaged pieces and missing records affect the decision. Do not repeatedly draw new samples until one passes. Any additional inspection should follow the agreed escalation or resampling rule, with the first result retained.
06 · Action thresholds
Agree how borderline results will be handled.
Write down the rule used to decide conformity, including how measurement uncertainty is considered. NIST’s discussion of conformity assessment explains that acceptance decisions and measurement uncertainty are connected, and that the decision rule involves business risk as well as technical measurement.
Distinguish specification limits from any inspection action threshold. If a guard band or a review zone is used, define it explicitly with the responsible technical party. A borderline reading should trigger the agreed review or verification step, not an improvised pass or automatic rejection.
Assign actions for confirmed nonconformity: identify and hold the affected scope where agreed, provide the raw readings and photographs, and discuss sorting, replacement or another documented resolution. Confirm who can approve an exception and keep that approval linked to the order.
07 · Verified order document
Put the agreed tolerance in the purchase record.
Request the current verified Unimax specification or technical document for the proposed grade. Confirm nominal dimensions, limits, measurement method, sample plan and edge-damage criteria. Connect the approved document version to the quotation, sample reference and intended packaging or HMD setup.
This guide invents no ideal tolerance range and publishes no unverified Unimax dimensional limit. The example is only an arithmetic illustration. A suitable order tolerance must be supported by relevant product evidence, functional requirements and an agreed measurement procedure.
Review the first identified samples using the same procedure intended for receipt inspection. Resolve gaps before release and retain the record for repeat orders. A practical tolerance is one that supplier and buyer can both measure and apply consistently.
Connect the result to the right product evidence.
Read the specification sheet and plan identified sample evaluation. Review cube density and dimensional measurement. Read the fixed-carbon panel guide, ash-content guide and moisture guide. Review current shisha product information and factory and quality evidence for the offered scope.
Technical references and scope
NPL — Callipers and micrometers, Good Practice Guide 40 supports the general discussion of measurement force, instrument use, verification and uncertainty. NIST — Assessment of Conformity, Decision Rules and Risk Analysis provides context for acceptance decisions and measurement uncertainty.
These are general metrology references, not shisha product specifications. The buyer procedure and illustrative numbers do not establish supplier certification or an ideal dimensional tolerance.
Before approving cube size tolerances
Does nominal size define the permitted variation?
No. Ask for explicit minimum and maximum limits and how they apply to length, width and height.
Why can zero-tolerance wording create disputes?
It leaves no stated allowance for production variation or measurement uncertainty. Agree measurable limits and a decision rule.
Can an average size prove every cube conforms?
No. Keep per-piece readings when the rule applies to individual pieces; use the agreed sampling and acceptance plan.
What should happen to a reading near a limit?
Apply the agreed uncertainty and borderline-review rule. Preserve the raw measurement and request verification when required.
Verified specification inquiry
Request the current technical data for your proposed order.
Send your country, buyer type, cube size, grade, application and volume. Ask Unimax for the verified specification or relevant technical document, with nominal dimensions, minimum and maximum limits, measurement points, sample count, edge-damage criteria and the acceptance rule identified.
Request verified technical dataReview current shisha products · Factory and quality evidence · Contact Unimax